In the current global industrial era, High Molecular Weight Polyacrylamide (PAM) stands as the backbone of environmental sustainability and resource recovery. As a synthetic resin prepared by polymerizing acrylamide, its water-soluble nature makes it indispensable. Oubo Chemical specializes in Cationic, Anionic, and Nonionic variants, providing high-performance solutions for secondary oil recovery, sewage treatment, and macromolecule separation.
Leveraging our location in the Free Trade Zone of Qingdao, China, Oubo ensures a robust global supplying chain. With raw materials sourced from Tier-1 suppliers like SINOPEC and Eni, we guarantee production stability even amidst global market fluctuations. Our annual capacity exceeded 50,000 Tons in 2018, ensuring we meet the demands of massive infrastructure projects worldwide.
Stringent global environmental regulations are driving the evolution of the water treatment industry. Oubo is committed to ISO9001:2008 standards, ensuring that our production processes minimize environmental footprints while maximizing polymer efficacy in applications like municipal sludge dewatering and industrial effluent clarification.
In the oilfield industry, PAM acts as a profile control agent and drilling fluid additive. It facilitates shale inhibition, lubrication of drill strings, and Enhanced Oil Recovery (EOR). Our high molecular weight polymers provide the necessary viscosity to displace oil in complex reservoirs.
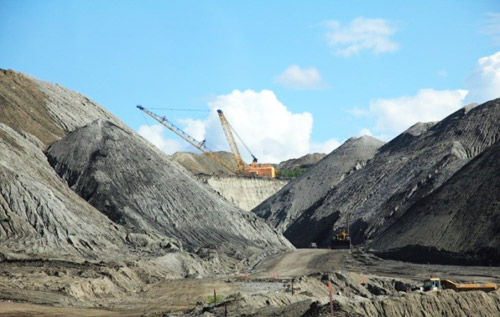
For coal washing and tailings treatment, Oubo PAM accelerates sedimentation and filtration. Our range includes varied ionic charges to suit mineral processing for Gold, Silver, Iron, and Copper, ensuring efficient tailing dewatering and pipe sealing.
Oubo serves the paper industry with dry strength agents and retention aids. By neutralizing anionic trash and forming covalent bonds with fiber hydroxyl groups, our polymers significantly improve paper quality and reduce raw material loss.
Qingdao OUBO Chemical Co, Ltd is a world leader, utilizing patented biological methods for PAM production. We invest €2 million annually into R&D to maintain technical superiority.
Our technical teams participate in the entire lifecycle—pre-sales testing, selection, and after-sales support—ensuring localized application success across different PH ranges and water types.
Our research focuses on "Green Polymers"—next-generation PAM that offers even higher biodegradable properties while maintaining superior flocculation strength to protect our planet.
Oubo ensures that product integrity is maintained from the factory to the site. We offer various packaging solutions including Blank bags, Normal bags, and Palletized shipping for international logistics efficiency.
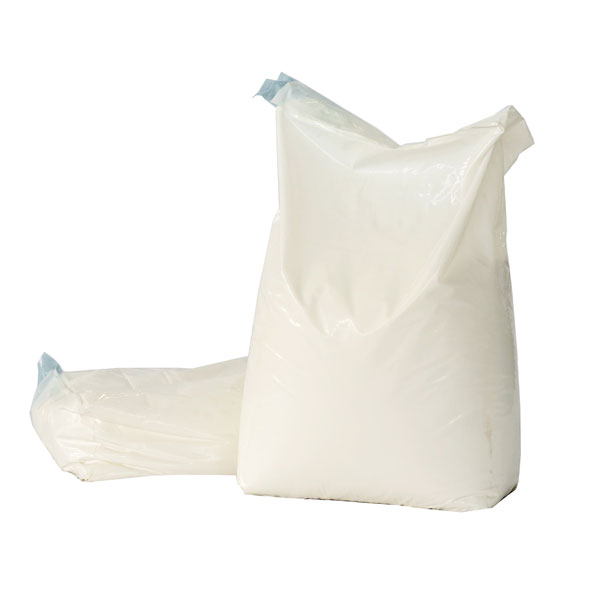
Standard Blank Bag
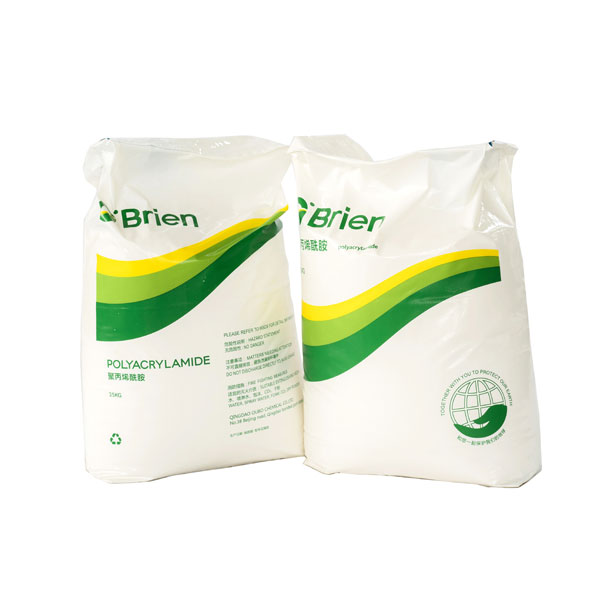
Normal Branded Bag
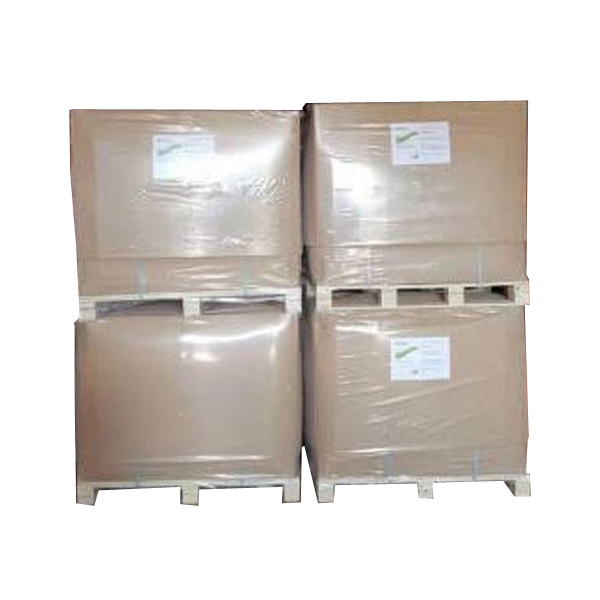
International Palletizing
It primarily acts as a flocculant, coagulant, and thickener. In wastewater treatment, it aggregates fine particles into larger flocs for easy removal. In EOR, it increases water viscosity to improve oil sweep efficiency.
We utilize an automated production line and a strict QC system where each batch is tested three times before delivery. We are ISO9001 certified and source materials from global leaders like SINOPEC.
Cationic (CPAM) is typically used for organic sludge (municipal), Anionic (APAM) for inorganic particles (mining/oil), and Nonionic (NPAM) for acidic wastewater or specific sugar refining processes. Our technical team can help you with free sample testing.
Yes. In the sugar industry, it is used for clarification and floatation. In textiles, it acts as a sizing agent, finishing agent, and for wastewater treatment to remove dyes.
 Oubo Chemical