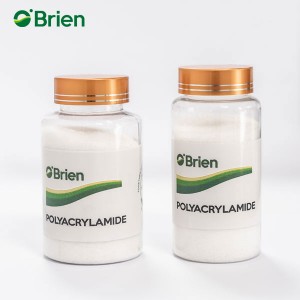
Explore our premium selection of industrial-grade flocculants and coagulants engineered for global standards.
Uncompromising standards in polymer manufacturing since 2011, located in the Qingdao Free Trade Zone.
Oubo Chemical Co., Ltd (O'Brien) has emerged as a premier global benchmark for PHPA, Sodium Acrylamide, and Copolymer solutions. Operating from the strategic Qingdao Free Trade Zone, our supply chain integrates premium raw material sourcing from elite global suppliers like SINOPEC and Eni. Our automated production lines and stringent 3-batch pre-delivery quality checks ensure unrivaled product reliability across international markets.
As global industrial demands shift toward stringent environmental compliance, modern enterprises require high-molecular-weight polymers that optimize efficiency while minimizing ecological footprints. Oubo’s revolutionary biological production methods and continuous R&D investment (exceeding €200 million annually) place us at the forefront of green polymer chemistry.
Embracing China’s Industry 4.0 evolution, our facilities leverage smart automation, real-time polymer monitoring, and precise reaction control systems. This technological leap eliminates batch-to-batch variance, granting global procurement managers absolute confidence in our Cationic, Anionic, and Nonionic Polyacrylamide formulations.
Whether deployed in enhanced oil recovery (EOR), municipal wastewater sludge dewatering, mineral processing, or paper retention, Oubo’s custom-engineered chemical auxiliary solutions deliver superior performance metrics under extreme industrial conditions.
Discover how our specialized polymer lines serve diverse industrial ecosystems worldwide.
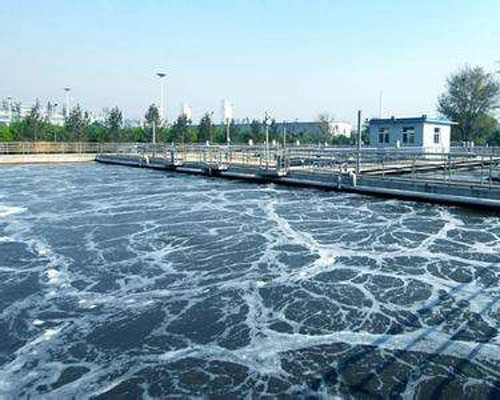
Extensively utilized in municipal and industrial solid-liquid separation, settlement, clarification, and sludge dewatering. Highly effective across leather, paper making, dyeing, and pharmaceutical wastewater.
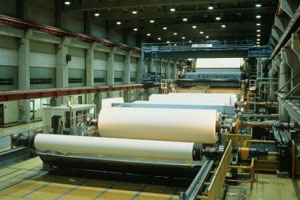
Functions as a premier dry strength agent, retention aid, and filter aid. Enhances physical paper strength, reduces fiber loss, improves white water treatment, and optimizes deinking efficiency.
Crucial in oil exploration, profile control, plugging agents, drilling fluids, and fracturing fluid additives. Reduces drilling fluid loss, provides shale inhibition, and lubricates drill strings.
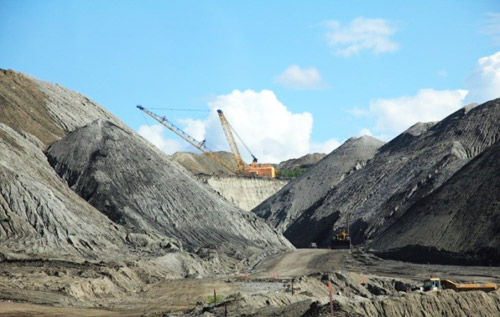
Essential for coal washing, tailing treatment, and solid-liquid separation via filtration/centrifugation in gold, silver, iron, nickel, and copper mineral processing.
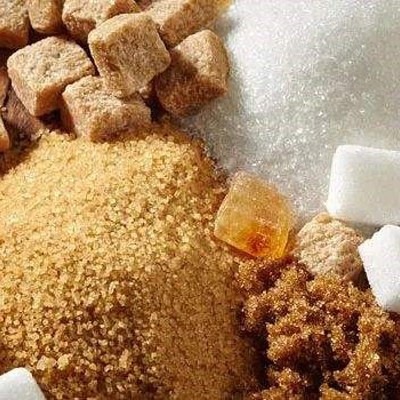
Employed in the clarification and flotation processes of sugar refining, ensuring high-purity food-grade processing standards and safe effluent handling.
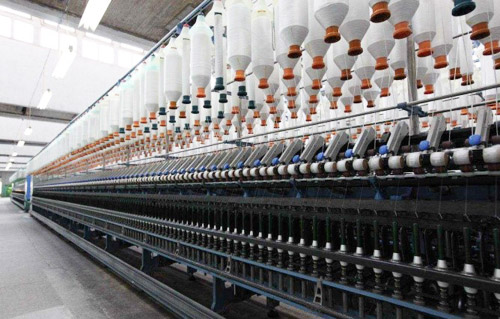
Acts as an advanced textile sizing agent, finishing agent, and fabric treatment chemical, providing exceptional anti-static properties and smooth fabric texture.
Our core competitive advantages built on innovation, strict QC, and dedicated technical service.
Pioneering biological methods for polyacrylamide production with patent-pending technology. Massive annual R&D investments ensure unmatched technical supremacy.
Global supply chain integration with ISO9001 compliance. Each production batch undergoes rigorous triple-testing by our expert QC team prior to dispatch.
Over a decade of specialized manufacturing expertise. Providing highly competitive pricing without ever compromising on superior molecular weight integrity.
End-to-end technical engagement covering pre-sales product selection, laboratory sample testing, and on-site troubleshooting after delivery.
Explore additional specialized grades and secure industrial packaging solutions.
Expert answers regarding PHPA, Sodium Acrylamide Copolymer, and Polyacrylamide applications.
 Wholesale Cationic Polyacrylamide Powder for Municipal & Industrial Wastewater Treatment Supplier, Suppliers
 Wholesale Nonionic Polyacrylamide (NPAM) for Mineral Processing & Metallurgical Ore Dressing Suppliers, Factories
 Wholesale PAM Anionic Polyacrylamide Manufacturer, Suppliers
 Wholesale Anionic Polyacrylamide Powder Flocculant for Food Processing & Sugar Refining Wastewater Manufacturer, Factories
 China Nonionic Polyacrylamide (PAM) Thickener for Oilfield Drilling Fluid Manufacturers, SuppliersChina Nonionic Polyacrylamide Manufacturers, Supplier
 China Cationic Polyacrylamide Retention & Drainage Aid for Paper Making Industry Supplier, Factories
 China Nonionic Polyacrylamide Flocculant for Acidic Industrial Wastewater Treatment Manufacturers, Factories
 Wholesale Cationic Polyacrylamide (CAS 9003-05-8) Flocculant for Textile & Dyeing Wastewater Manufacturer, SupplierWholesale Anionic Polyacrylamide Manufacturers, Supplier
 Wholesale High Molecular Weight Anionic Polyacrylamide for Petrochemical & Metallurgical Wastewater Suppliers, FactoriesChina PAM Anionic Polyacrylamide Dry & Wet Strength Agent for Paper Industry Manufacturers, FactoriesChina Cationic polyacrylamide Manufacturer, Supplier
 Wholesale Anionic Polyacrylamide (APAM) for Municipal Sewage Treatment & Sludge Dewatering Manufacturers, Suppliers
 Wholesale Cationic Polyacrylamide (CPAM) for Sludge Dewatering & Industrial Wastewater Flocculation Supplier, Factories
 Wholesale High Molecular Weight Nonionic Polyacrylamide for Coal Washing & Tailings Dewatering Manufacturers, Suppliers
Oubo Chemical Co., Ltd was established in 2011, located in Qingdao Free Trade Zone. Annual capacity over 50,000 Tons. ISO9001:2008 certified. Specializing in Cationic, Anionic, and Nonionic Polyacrylamide, serving Waste Water Treatment, Oil & Gas Extraction, Mining, Agriculture, Paper & Pulp, Paints & Coatings, Textiles, Food, and others.
 Oubo Chemical